In the dynamic landscape of the global chemical industry, acetic acid stands as a versatile and high-demand organic intermediate, underpinning the production of countless downstream products from plastics to pharmaceuticals. As a leading chemical turnkey engineering provider, Jiangsu Huda Chemical Technology Co., Ltd. has honed its acetic acid plant technology through years of R&D and project practice, crafting tailored, high-performance production solutions that align with the industry's push for sustainability and efficiency. Huda Chemical Technology's acetic acid technology is not just about building plants—it's about building reliable, low-cost, and eco-friendly production systems that empower customers to thrive in a competitive market.
Acetic Acid's Unmatched Role in Modern Chemical Production
Acetic acid is far more than a basic chemical raw material; it's a critical building block for over 80% of the fine and specialty chemicals that drive daily life, from vinyl acetate for adhesives to terephthalic acid for polyester fibers, and even pharmaceutical intermediates and new energy materials. For chemical manufacturers, the quality and efficiency of acetic acid production directly impact production costs, product quality, and market adaptability.
Conventional acetic acid production processes often suffer from high energy consumption, unstable catalyst performance, and complex post-treatment systems, leading to elevated operational costs and environmental risks. Huda Chemical Technology, leveraging its profound technical accumulation in chemical engineering, has targeted these pain points to optimize every link of acetic acid production. By integrating advanced process design and intelligent control, the company's acetic acid plant technology ensures high-purity output (≥99.85%) while cutting energy use and reducing waste emissions, making it a go-to choice for global customers pursuing green and efficient production. As the demand for high-purity acetic acid surges across industries, Huda Chemical Technology's proven technology provides a solid foundation for customers to scale production and capture market opportunities.
What Makes Huda Chemical Technology's Acetic Acid Production Process Stand Out?
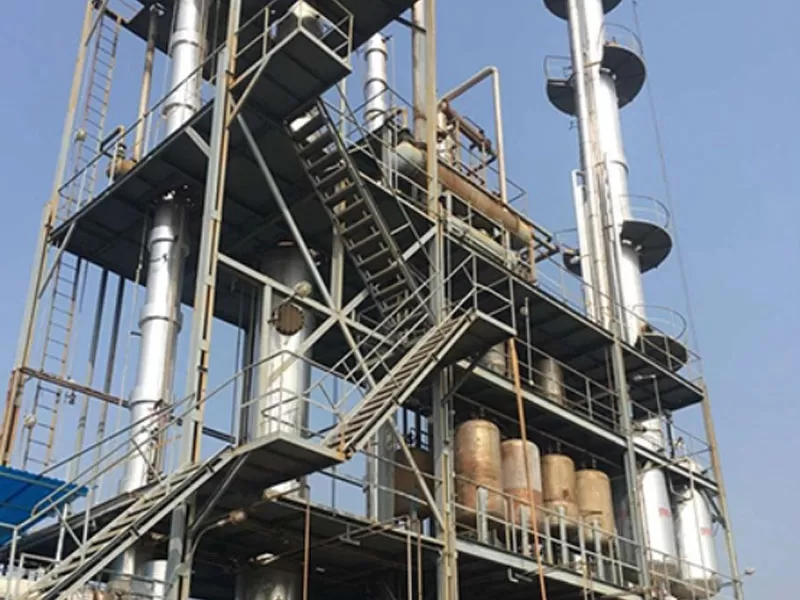
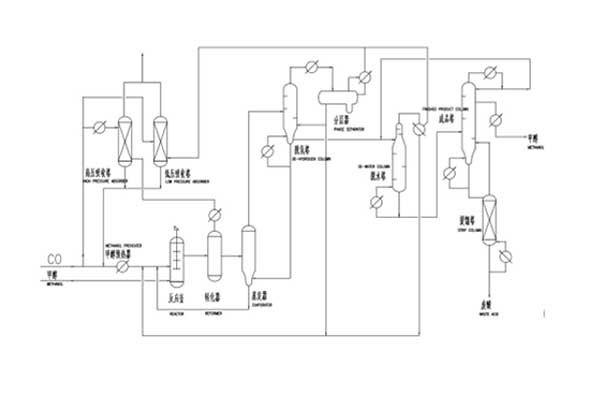
The core of Huda Chemical Technology's acetic acid plant technology lies in its optimized methanol carbonylation process, a mature and industry-recognized synthesis route that the company has upgraded with proprietary design and technical tweaks. Taking methanol and CO as raw materials, the process synthesizes acetic acid continuously under mild reaction conditions (3.0MPa(G), 180–220℃) with a rhodium-based catalyst, and the crude product is purified to high purity through a sophisticated distillation system—all while boasting advantages that set it apart from traditional processes:
Superior Catalyst Performance: The customized rhodium catalyst features higher stability, activity, and selectivity, enabling long-term continuous production without frequent replacement, which slashes catalyst costs and reduces production downtime.
Streamlined Process & Low Investment: The simplified process flow requires fewer pieces of key equipment, lowering initial construction investment and shortening project construction cycles—ideal for both new plant construction and existing plant upgrades.
Energy-Saving & Eco-Friendly Operation: Advanced heat integration technology recycles waste heat from the reaction and distillation processes, minimizing external energy input and cutting overall energy consumption. A comprehensive by-product recovery system collects and treats hydrogen, CO2, and unreacted raw materials, meeting strict environmental emission standards and realizing resource recycling.
High Safety & Long-Term Stability: The entire production system is equipped with DCS, SIS, and ESD intelligent safety control systems, and over 80% of the core equipment uses corrosion-resistant zirconium materials. This dual protection of equipment material and intelligent control ensures safe, stable, and long-cycle operation of the acetic acid plant.
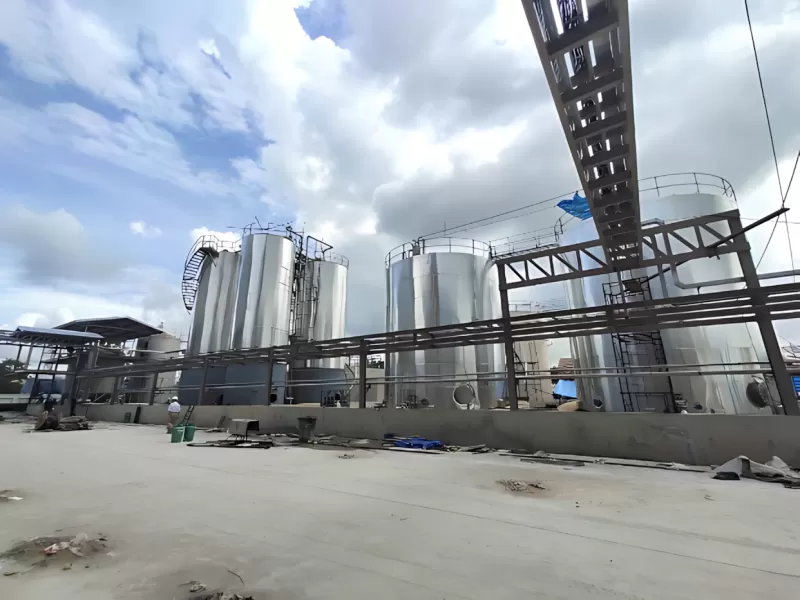
Modular Design for Fast Commissioning: Adopting modular skid-mounted design for key process units, Huda Chemical Technology reduces on-site installation and debugging work, accelerates project delivery and commissioning, and helps customers put plants into production quickly to generate revenue.
Every optimization of Huda Chemical Technology's acetic acid process is centered on customer needs—whether it's reducing production costs, improving product purity, or enhancing environmental performance, the technology delivers tangible value for global chemical enterprises.
Future Trends Shaping Acetic Acid Plant Technology
As the chemical industry accelerates its shift toward low-carbon and circular development, acetic acid plant technology is evolving in tandem with two core trends: higher integration and raw material diversification. Huda Chemical Technology is at the forefront of these trends, integrating its core strengths in distillation technology and air separation units (ASUs) into acetic acid plant design—its high-integration air separation technology provides high-purity CO raw material for acetic acid synthesis, while advanced distillation optimization further boosts the efficiency of acetic acid purification, realizing the seamless integration of upstream and downstream processes in the plant.
In terms of raw material diversification, the industry is increasingly exploring sustainable raw material routes, such as using CO2 captured from industrial emissions as a supplementary raw material for acetic acid synthesis. Huda Chemical Technology is already researching and developing this low-carbon technology, combining its existing process advantages with carbon capture and utilization (CCU) technology to explore a more eco-friendly acetic acid production route. Additionally, the company is continuously integrating intelligent manufacturing technology into acetic acid plants, realizing real-time monitoring and automatic adjustment of production parameters, which further improves production efficiency and reduces human operational errors.
For Huda Chemical Technology, the future of acetic acid plant technology is about balancing efficiency, sustainability, and flexibility—creating production systems that not only meet current market demands but also adapt to future industry upgrades and environmental regulations.
Conclusion
Acetic acid plant technology is a key pillar of the modern chemical industry's development, and Jiangsu Huda Chemical Technology Co., Ltd. has established itself as a reliable partner for global customers with its optimized, customer-centric acetic acid production solutions. By refining the methanol carbonylation process, integrating energy-saving and safety technologies, and keeping pace with industry low-carbon and integration trends, Huda Chemical Technology's acetic acid plant technology delivers more than just high-purity acetic acid production—it delivers stable operation, low costs, and sustainable development capabilities for customers.
As a professional chemical turnkey engineering service provider, Huda Chemical Technology combines its acetic acid technology with its full-chain service capabilities, from plant design and equipment manufacturing to installation, commissioning, and after-sales support, providing one-stop solutions for global customers. Looking ahead, Huda Chemical Technology will continue to deepen R&D in acetic acid plant technology, explore low-carbon raw material routes and intelligent manufacturing applications, and work hand in hand with chemical enterprises worldwide to drive the sustainable and high-quality development of the acetic acid industry, redefining efficiency and sustainability in chemical manufacturing.